Workpiece & Challenge
Crankshafts are typically forged steel or ductile iron with high hardness and toughness. The most difficult operation is deep oil-hole drilling (often above 10xD), where chips can jam and exit quality can become unstable.
Automotive deep-hole drilling solution with solid carbide coolant-thru twist drills
This case focuses on long-depth oil-hole machining on crankshafts, where stable chip evacuation, tool life, and hole quality are critical in mass production.
Crankshafts are typically forged steel or ductile iron with high hardness and toughness. The most difficult operation is deep oil-hole drilling (often above 10xD), where chips can jam and exit quality can become unstable.
Use customized solid carbide coolant-thru twist drills with MQL (minimum quantity lubrication) to improve chip evacuation stability, lower coolant and maintenance costs, and support cleaner production.
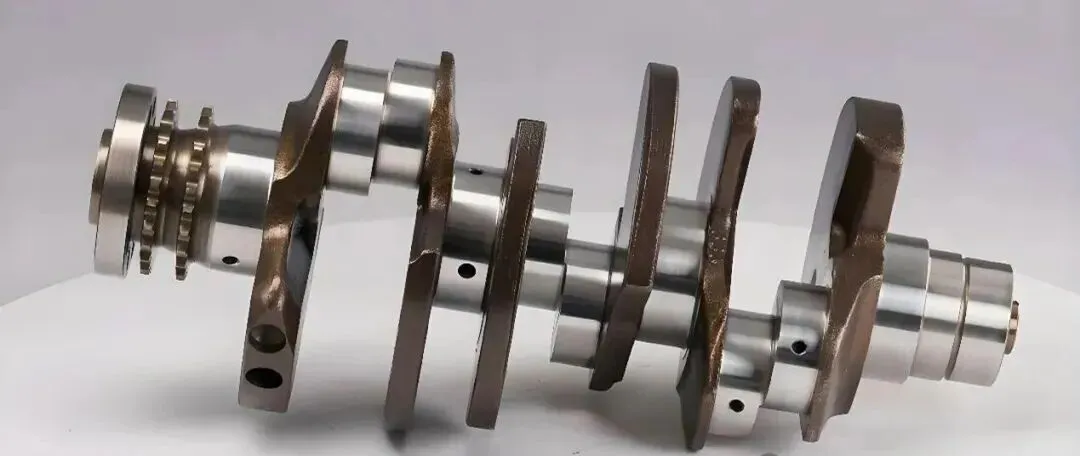
Crankshaft
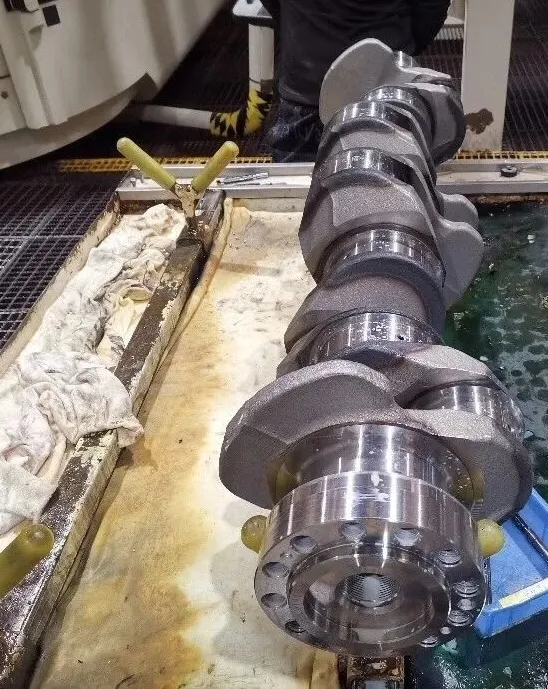
Crankshaft by our drills
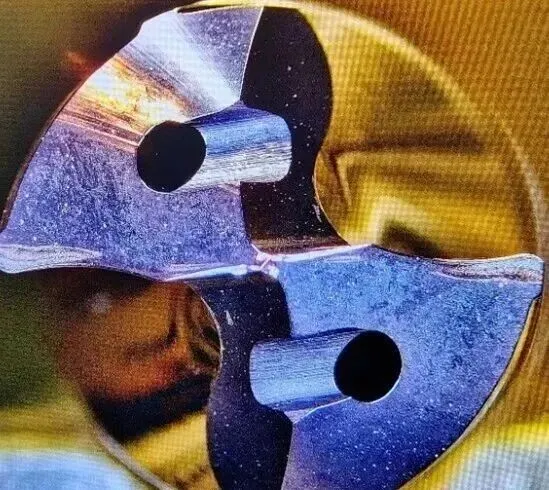
Our drill design optimized for crankshaft
| Condition | N(RPM) | Vc(m/min) | Vf(mm/min) | Fn(mm/r) | Lifetime (holes) | Lifetime (meter) | Result |
|---|---|---|---|---|---|---|---|
| Before (Competitor) | S2800 | 70 | F616 | 0.22 | 800 Holes (unstable, easy to break) | 63m | - |
| After (KY TOOLS) | S2800 | 70 | F616 | 0.22 | 1720 Holes | 136m | 115% longer tool life. More consistent. Better value than comparable brands. |