被削材 & Challenge
Crankshafts are typically forged 鋼 or ductile iron with high 硬さ and 破壊靭性. The most difficult operation is deep oil-hole drilling (often above 10xD), where chips can jam and exit quality can become unstable.
Automotive deep-hole drilling solution with 超硬ソリッド coolant-thru ツイストドリル
This case focuses on long-depth oil-hole machining on crankshafts, where stable chip evacuation, tool life, and hole quality are critical in mass production.
Crankshafts are typically forged 鋼 or ductile iron with high 硬さ and 破壊靭性. The most difficult operation is deep oil-hole drilling (often above 10xD), where chips can jam and exit quality can become unstable.
Use customized 超硬ソリッド coolant-thru ツイストドリル with MQL (minimum 数量 lubrication) to improve chip evacuation stability, lower coolant and maintenance costs, and サポート cleaner production.
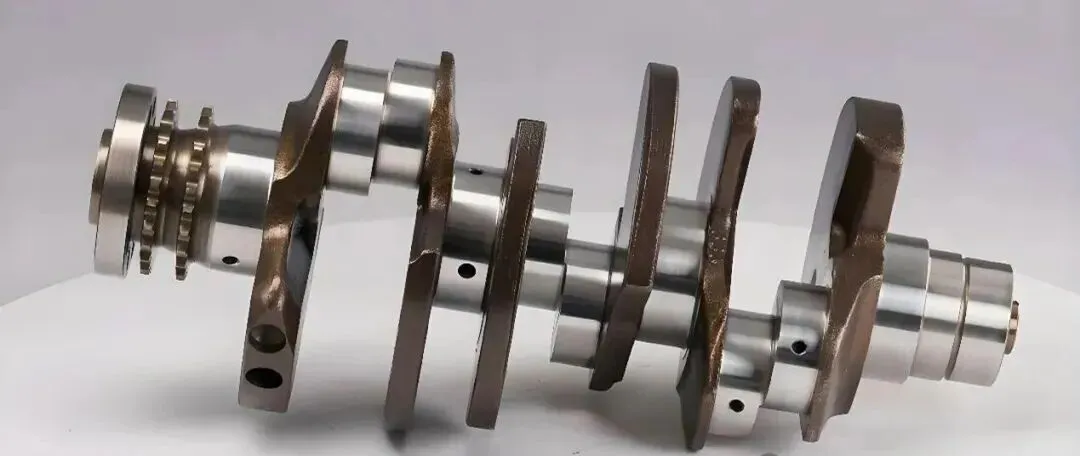
Crankshaft
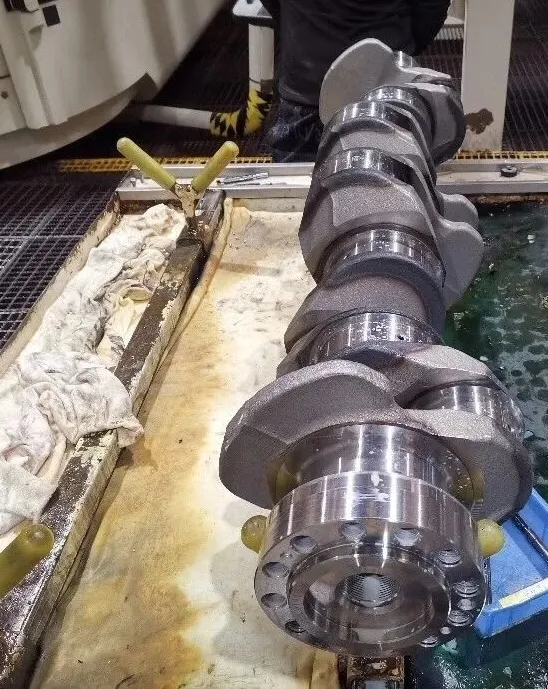
Crankshaft by our ドリル
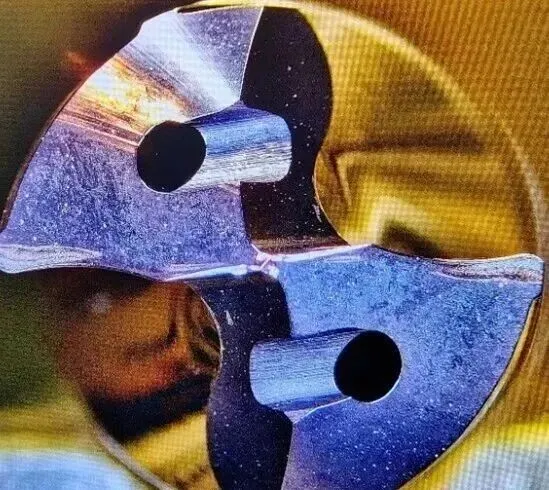
Our drill design optimized for crankshaft
| Condition | N(RPM) | Vc(m/min) | Vf(mm/min) | Fn(mm/r) | Lifetime (holes) | Lifetime (meter) | Result |
|---|---|---|---|---|---|---|---|
| Before (Competitor) | S2800 | 70 | F616 | 0.22 | 800 Holes (unstable, easy to break) | 63m | - |
| After (KY TOOLS) | S2800 | 70 | F616 | 0.22 | 1720 Holes | 136m | 115% longer tool life. More consistent. Better value than comparable brands. |